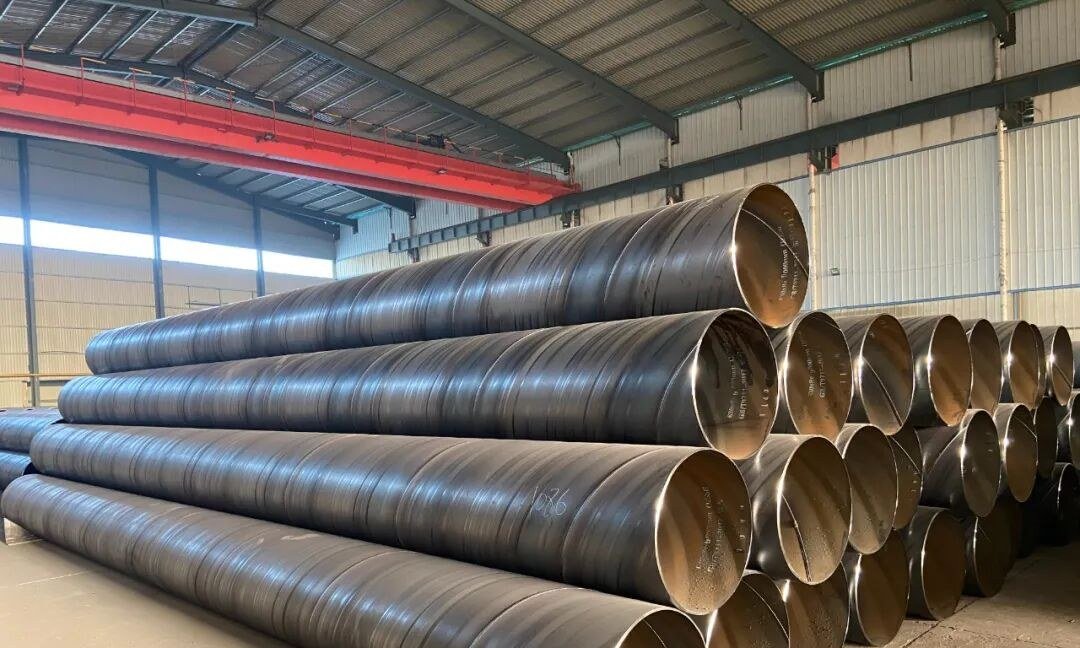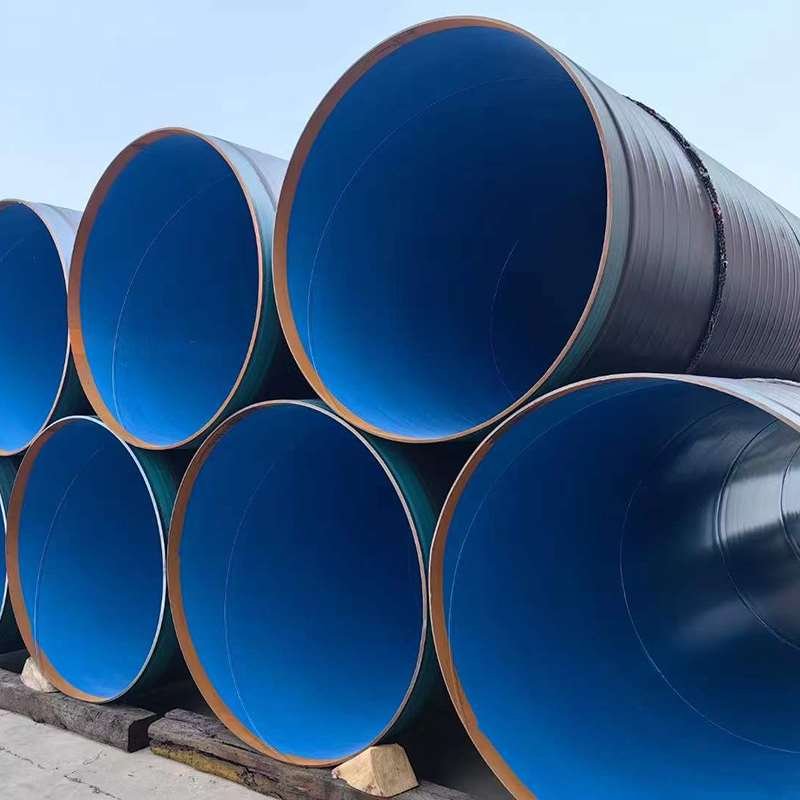
MCC Saindak Copper-Gold Project — 38,000 m DN600 Pipe
38,000+ m of DN600 cement-mortar-lined spiral pipe; 325 truckloads to port in two months and 40 days of on-site support in Pakistan.
Read full case →Representative deliveries across five application areas — from mine-site water supply to offshore piling. Each one lists the actual specification, inspection and logistics, so you can judge fit line by line.
Six representative orders, grouped by what the pipe had to do rather than by date — so you can find the closest match to your own project. No client logos we cannot show — only specifications and records that exist.
38,000+ m of DN600 cement-mortar-lined spiral pipe; 325 truckloads to port in two months and 40 days of on-site support in Pakistan.
Read full case →
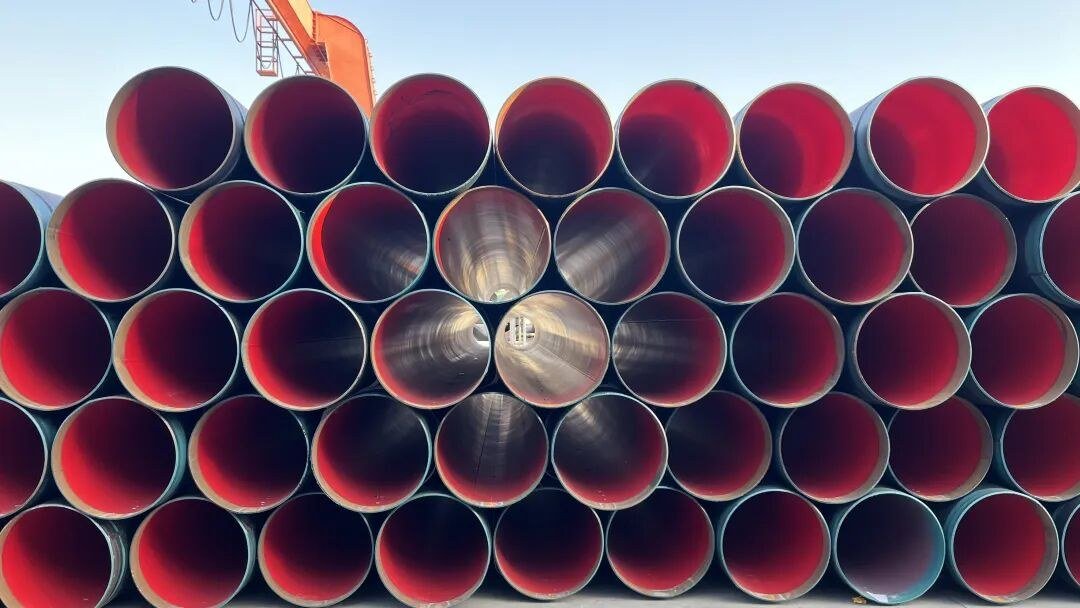
D610 and D813 TPEP pipe with spherical socket lap-weld and red epoxy lining — accepted by five parties, installed in early 2025.
Read full case →
DN1600–DN2000 spiral pipe with internal and external epoxy, 100% UT and RT on every weld and a hydrostatic test on every pipe.
Read full case →
20,000+ m of anti-corrosion ERW pipe across 2,400+ pipes and thousands of fittings, moved in 240+ truckloads within one month.
Read full case →
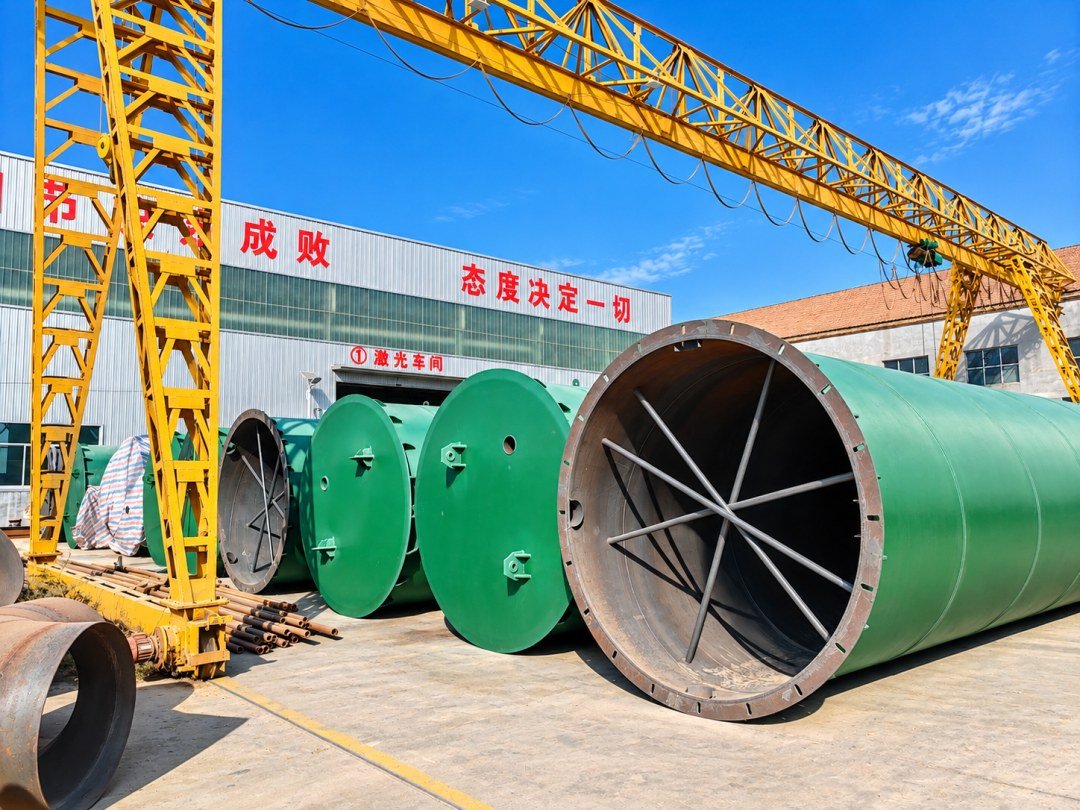
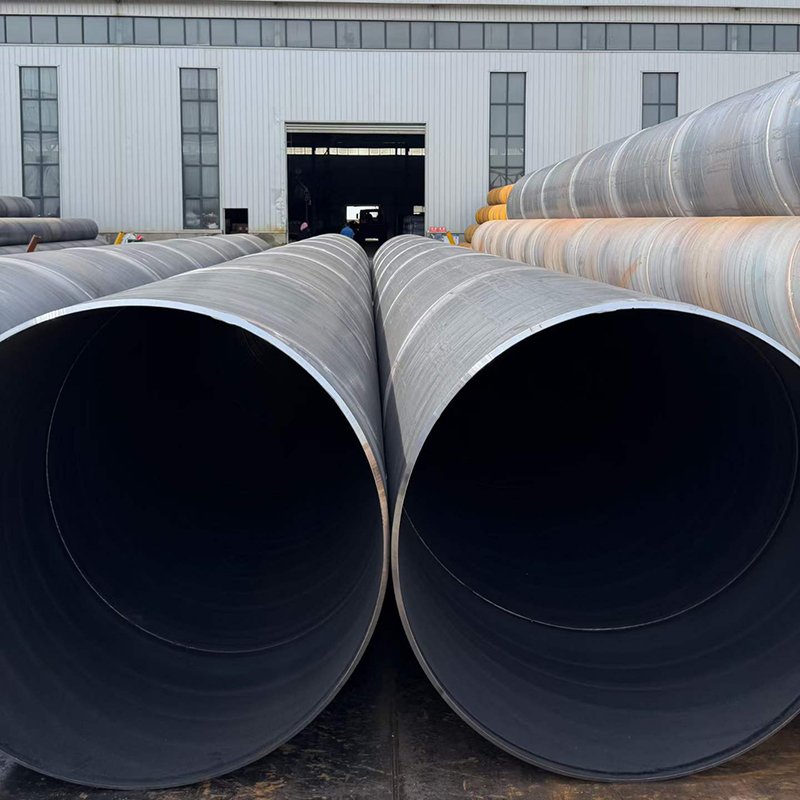
2500 mm Q355C anti-corrosion spiral pipe plus supports, stiffeners and flanges — SGS-witnessed UT, first article approved, 15-day manufacture.
Read full case →
5,000 m of 508 and 813 mm heavy-wall FBE piling pipe with full-length coating and 100% X-ray RT, dispatched 19 October 2026.
Read full case →Additional written-up projects by destination — coating system and standard matched to local water chemistry, soil and inspection practice.
Why 3LPE external coating plus an internal lining is the working combination for provincial water mains in the Philippines.
Read the full case →
Fusion-bonded epoxy for plant piping in Vietnam and Thailand — potable-water lining, fittings and flange faces included.
Read the full case →
How AWWA C210 lining and coating is specified and inspected on large-diameter water mains in Malaysia.
Read the full case →Coating and logistics only matter if the pipe body and weld are sound. Every order runs on a documented inspection and test plan (ITP) — a ten-step programme agreed before production starts, with 100% UT and RT on the weld and a hydrostatic test on every pipe.
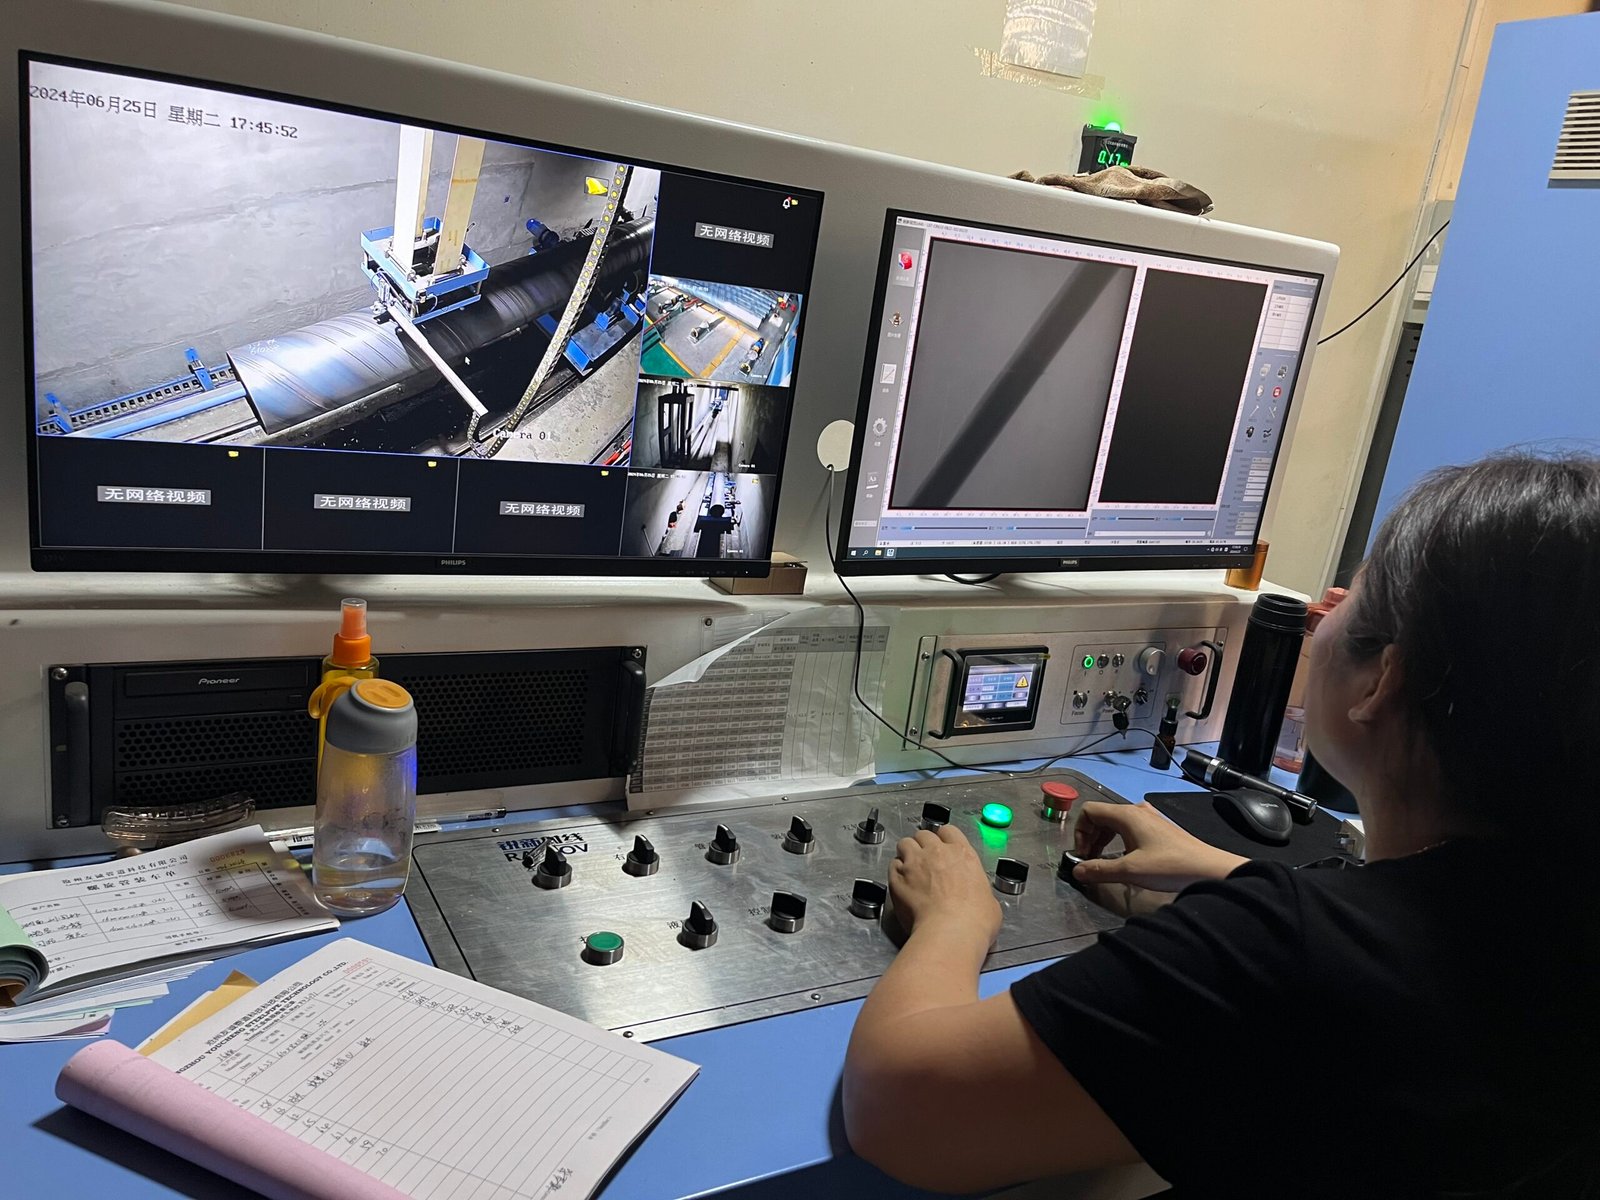
X-ray examination of the spiral seam. On critical water mains RT runs alongside 100% in-line ultrasonic testing, so the weld is checked by two independent methods.
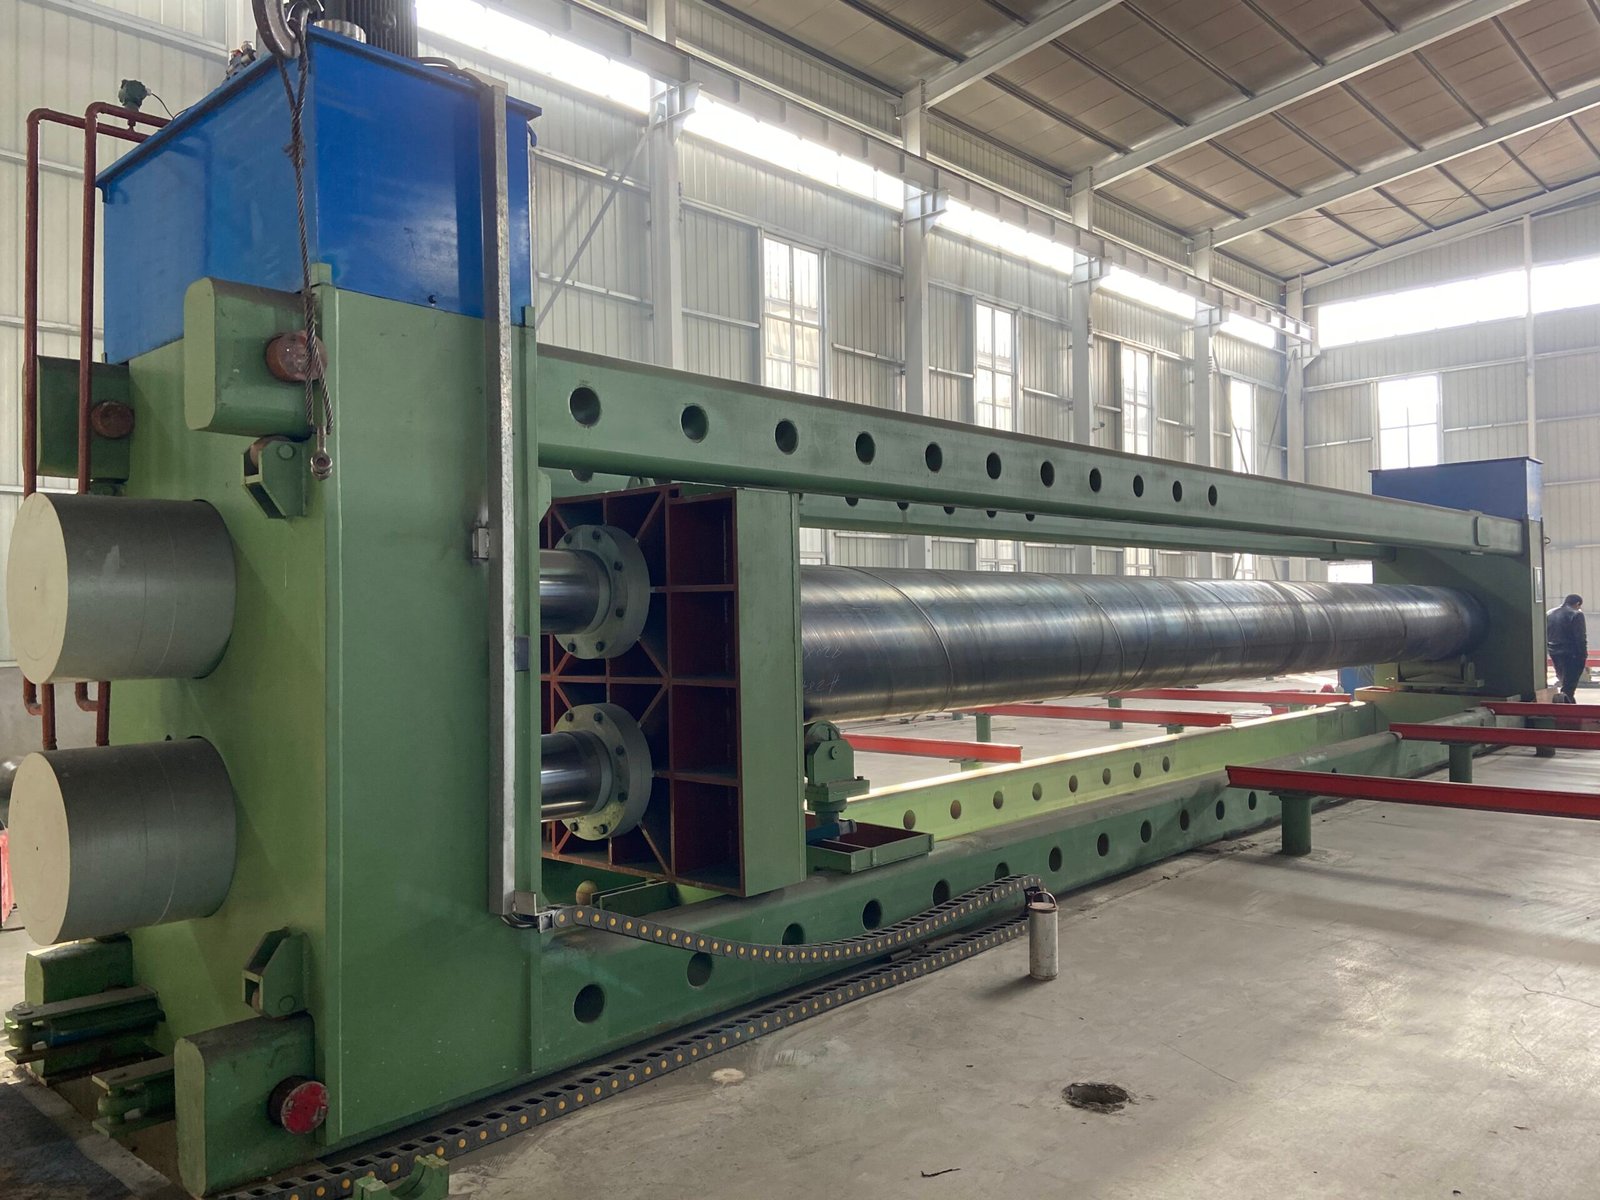
Every pipe is pressure tested and held to the specified test pressure and hold time, with the gauge reading recorded against the pipe number.
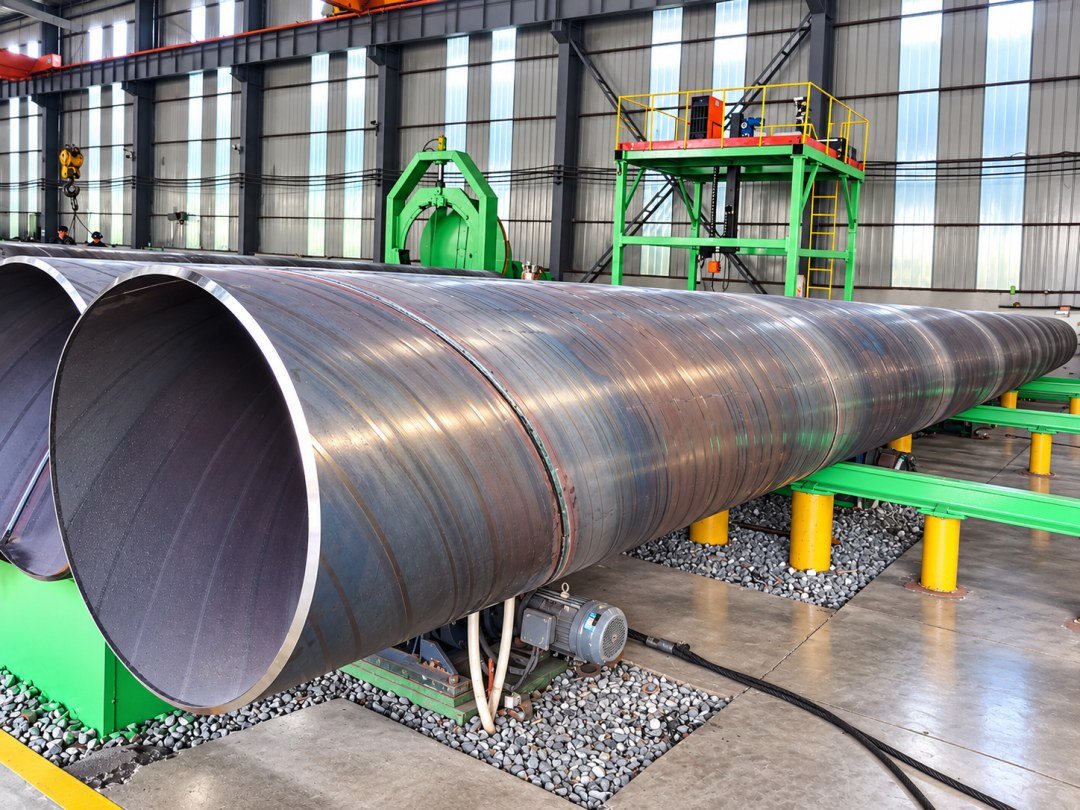
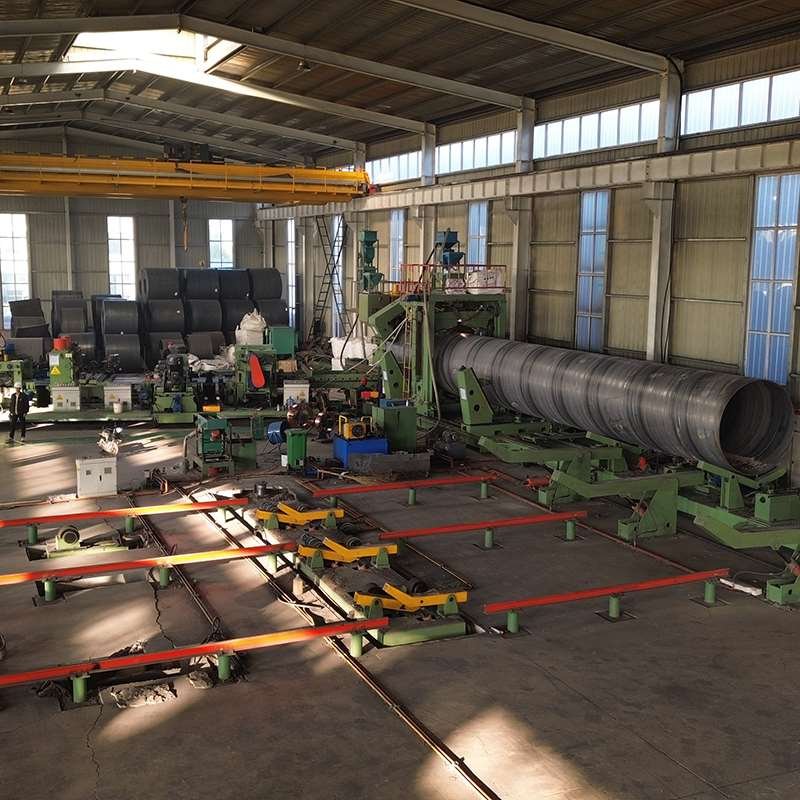
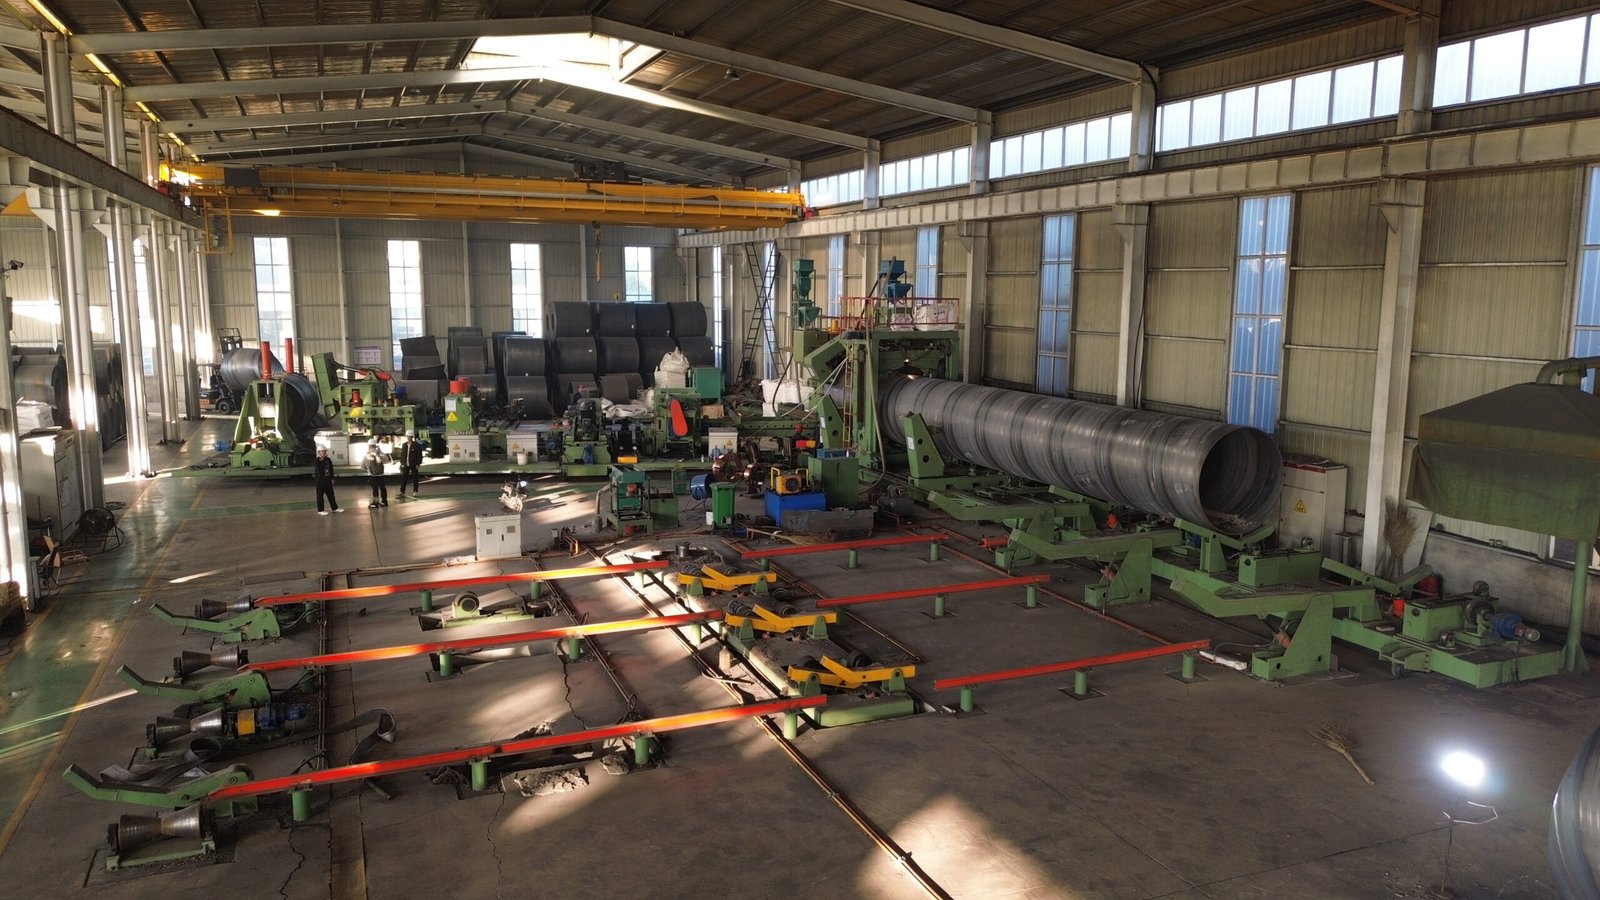
Coil is formed and seam-welded on the spiral line, then sized and end-prepared. Diameter and wall thickness are checked against the order before coating begins.
Coating, lining, marking and end protection happen on the same site as the mill — so a coated pipe never travels between suppliers before it reaches the port.
Need the full standard comparison behind these specifications? Steel Pipe Standard & Coating Selection Matrix →
Send the OD, wall thickness, standard, coating system and destination port. We will come back with the pipe schedule, inspection plan and shipping arrangement — the same way these projects started.